IPC Class 3 PCB Assembly: Inspection, Scheduling and Cost Factors
Class 3 assembly tightens solder acceptance and calls for inspection matched to each joint, with parts, first articles and test readiness shaping delivery.
IPC Class 3 assembly puts tighter workmanship limits and documented inspection at the center of a build. On one board, that can mean measuring exposed controller leads, checking connector joints inside plated holes and examining solder balls hidden beneath a BGA. The inspection plan needs to match each connection and the acceptance requirements agreed for the specific assembly.
EBest Circuit says its engineers review designs before production at its PCB and assembly factories, providing a design-for-manufacture report and a bill of materials optimization list. For fine-pitch BGAs, that review can flag a footprint mismatch before parts are ordered and identify joints that require X-ray inspection. The company asks customers to provide assembly drawings and BOMs for an engineering review and turnkey quote.
Where Class 3 requirements apply
Class 3 may be specified for assemblies expected to operate continuously or respond reliably when called on. Examples include flight control computers, satellite telemetry boards, ventilator controllers, pacemaker pulse generators, MRI acquisition boards, airbag control units, railway signaling interlocks, protective relay boards, emergency-stop controllers and subsea instrument controllers.
The product owner sets the class for each assembly. A patient monitor’s alarm board and an accessory for the same product, for example, may have different acceptance requirements. A Class 3 bare PCB specification also doesn’t automatically establish the acceptance class for the populated assembly: component placement, solder joints and finished workmanship need their own assembly requirements.
A tighter limit can change acceptance
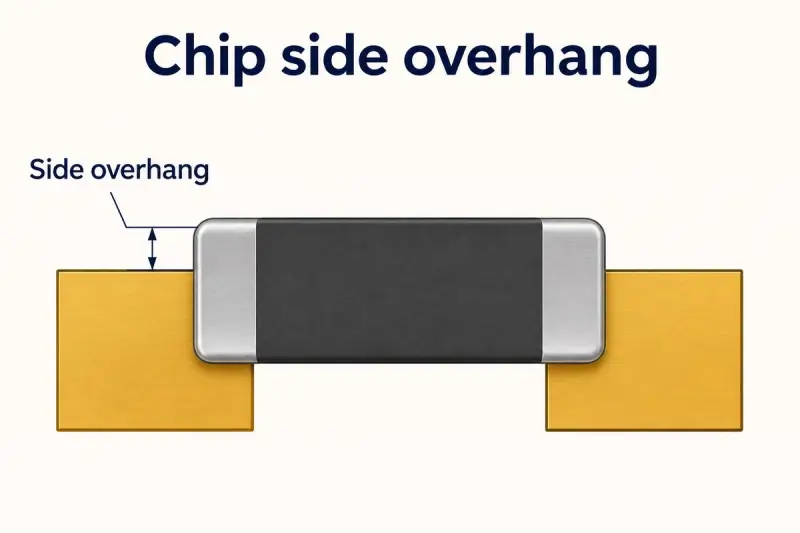
The difference between Class 2 and Class 3 can be significant even when a board powers up. Under the side-overhang criterion in IPC-A-610E §8.3.2.1, the narrower of a chip termination and its pad sets the reference width. For a 0.40 mm termination on a 0.50 mm pad, that reference is 0.40 mm.
| Side overhang | Class 2 | Class 3 |
|---|---|---|
| Maximum as a share of reference width | 50% | 25% |
| Maximum for this chip | 0.20 mm | 0.10 mm |
| Measured overhang of 0.15 mm | Within limit | Exceeds limit |
The example shows why acceptance should be tied to the revision and criteria specified for the order. The cited limits describe revision E; production evaluation follows the revision invoked by the controlling documents and the requirements for the actual termination.
Inspection must fit the joint
J-STD-001 addresses soldering materials and processes; IPC-A-610 provides workmanship criteria for evaluating the completed assembly. EBest Circuit describes matching inspection to the connection type:
| Connection | Inspection focus |
|---|---|
| Gull-wing lead | Side overhang, joint width and heel fillet |
| Through-hole pin | Barrel fill, wetting and land coverage |
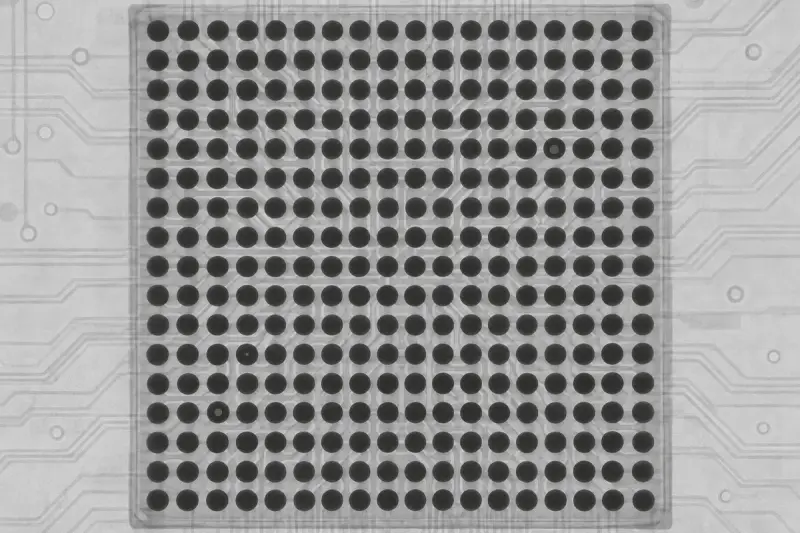
| BGA solder balls | Alignment, bridges and void patterns |
Optical inspection can reveal a displaced exposed lead or a bridge between visible pins. At a through-hole connector, the surface fillet shows wetting at the board face, but it may not show how much solder filled the barrel. That requires a separate evaluation when the fill can’t be assessed from the visible side.
BGA joints need a method that can see through the package. X-ray can reveal a bridge beneath it, while functional testing can establish whether a processor boots and communicates under specified conditions. When both are required, the inspection agreement should identify packages, X-ray acceptance criteria, sampling and records retained for each lot or serial number.
What sets delivery time and cost
EBest Circuit gives 10–12 business days from confirmed files and purchase order as a general turnkey PCBA planning reference. For a Class 3 order, the ship date also depends on the complete parts kit, first-article approval and readiness of required tests. PCB fabrication and component sourcing can proceed in parallel, but a late processor can delay SMT assembly, while a missing through-hole connector can hold shipment after SMT is done. A customer review of the first assembled board and late test fixtures or firmware can also extend the schedule.
On repeat orders, an unchanged board revision and test procedure may allow existing setups to be reused. Quotes should distinguish the first-article ship date from the tested production-lot ship date.
Cost depends on which charges recur per board and which cover shared setup. A stencil or dedicated fixture may serve multiple batches if the design remains compatible; spreading the same fixture charge across 200 boards rather than 20 reduces its per-board share to one tenth. Each unit still needs its own parts and assembly time. Through-hole power connectors add a soldering operation after the surface-mount stage when that sequence is specified.
Inspection coverage affects price too. Reviewing a BGA on every board and retaining an image linked to its serial number takes more work than sampling a lot. Two quotes for the same BOM can therefore include different levels of inspection and record keeping.
Example: portable diagnostic device
A Mexico-based medical device manufacturer commissioned EBest Circuit to assemble a 12-layer HDI board for a portable diagnostic device. The design used 01005 components and BGAs. The project specified IPC-A-610 Class 3 workmanship and a separate BGA void target of 3% or less.
EBest Circuit reports controlling solder-paste deposition for the small 01005 pads, then using 3D X-ray after reflow to evaluate voiding against the project target. It also captured process records in a manufacturing execution system, giving the customer’s quality team a way to trace an individual board’s production history. The example shows how a project-specific void target can sit alongside a workmanship class, with inspection records supporting later review.
Requirements to settle before production
For a quote, EBest Circuit requests Gerber or ODB++ files, a BOM with manufacturer part numbers, placement data and the released assembly drawing. Customers should identify the applicable standards, revisions and class, critical BGAs by reference designator, and any X-ray, firmware or functional test requirements. Prototype and repeat quantities, customer-supplied parts, and target dates for first articles and completed lots help define scope and schedule.
Project documents can assign different acceptance classes to prototypes and production boards. A prototype accepted to Class 2 may support firmware development, while production qualification to Class 3 calls for evidence from a build evaluated to those criteria. If an older drawing remains in use, the controlling order and drawing should agree on the revision; any move to a newer revision needs agreement.
An inspector’s IPC training certificate describes that person’s qualification within its stated scope. Shipment evidence must still apply to the supplied assemblies, their revision and the order’s acceptance requirements. Likewise, a functionally equivalent alternate component can have different termination geometry, moisture handling or reflow limits. Engineering review determines whether assembly settings, inspection programs or first-article checks need updating before it enters production.
EBest Circuit says it supports prototypes and small batches, and offers a 1.5-week PCBA turnaround for eligible builds when parts and test requirements are ready. It also says its digital shop floor can retrieve recorded material and product batch details within five seconds. For a practical schedule and price, the key is to provide the released files and define inspection coverage, first-article approval and test readiness before the build begins.
 AMD Venice Uses 2.5D Packaging to Feed More Bandwidth Into EPYC Zen 6
 CNC Controller Board Design: Interfaces, PCB Specs and Assembly Testing
 Stratasys and Nano Dimension End $42.5 Million Markforged Sale Agreement