Surface Mount PCB Assembly: Process, Inspection and Design Limits
EBest Circuit supports 01005 parts and 0.25 mm BGA pitch, with assembly scope and inspection set by the board’s design and test needs.
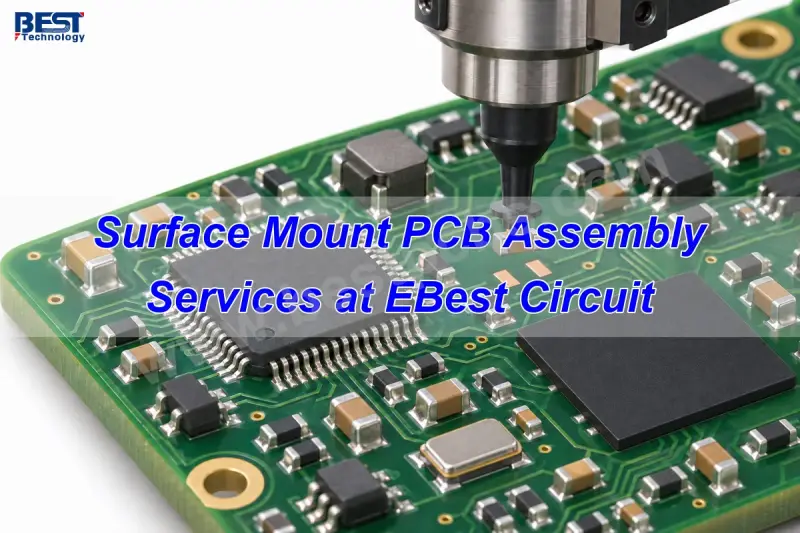
Surface mount assembly quality depends on a chain of linked decisions: footprint and stencil design, paste printing, component placement, reflow, and inspection. EBest Circuit describes a service covering those production steps, with component sourcing, PCB fabrication, through-hole assembly, programming, and functional testing available according to the agreed project scope.
The stated placement range includes 01005 surface mount components and BGA packages with pitch down to 0.25 mm. Those figures describe documented capabilities, not automatic acceptance of every board using those packages. The actual layout, component drawing, handling needs, and inspection plan still determine whether a particular assembly is manufacturable.
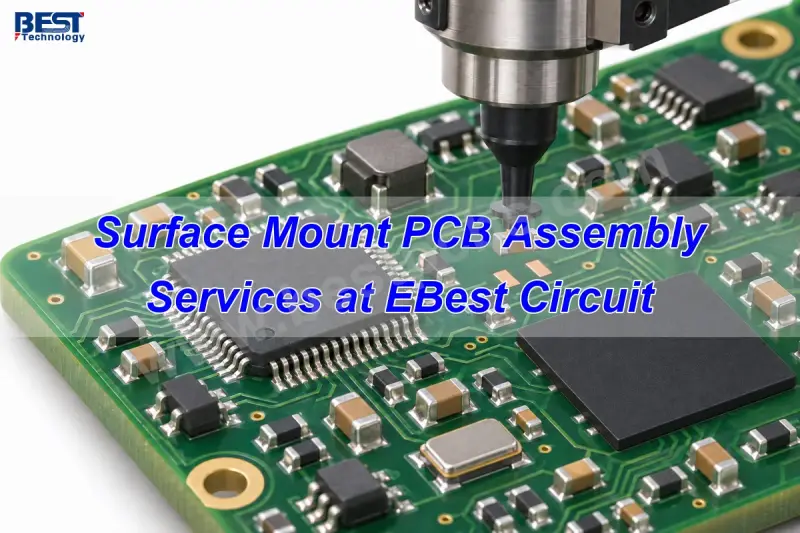
Assembly scope and component formats
The service covers stencil preparation, paste printing, SMT placement, reflow, and inspection. Customers can provide selected parts, supply all components, or request sourcing as part of a partial or full turnkey build. Boards can be SMT only or combine surface mount parts with through-hole components.
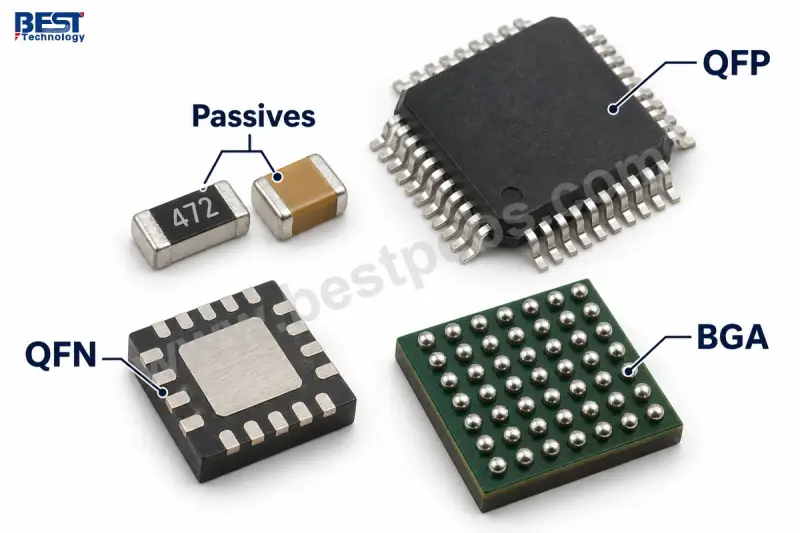
The listed package families include chip resistors and capacitors, diodes, transistors, SOIC, QFP, QFN, and BGA. Component presentation can include reels, cut tape, tubes, trays, or loose parts, subject to handling review. The form in which parts arrive affects preparation: identification, packaging condition, moisture sensitivity, and quantity available for setup all matter.
Small parts and dense packages call for more than a placement machine capable of reaching their nominal size. A 01005 passive beside a tall connector may restrict nozzle access or make inspection harder than the same part in an open area. EBest Circuit says it reviews the populated board and package details together, rather than treating the smallest component as sufficient evidence that the full design is ready.
Package details shape the process
Different component families create different manufacturing and inspection problems. Chip passives need balanced pads and paste deposits to reduce skew and tombstoning. SOIC and QFP packages depend on lead coplanarity, alignment, and separation between fine-pitch paste deposits to avoid bridges or open joints.
QFN packages add an exposed thermal pad beneath the body. Its stencil aperture pattern needs to account for both the center pad and the perimeter lands; excess paste under the center can lift the package or interfere with perimeter joints. BGA process planning depends on ball pitch, land pattern, board warpage, and the reflow profile. Because the solder joints are hidden, ordinary top-side optical inspection cannot establish their condition.
Footprints should be checked against the exact manufacturer package drawing and approved part number. Devices with matching pin counts can still have different body dimensions or land patterns. The design review also considers solder mask, fiducials, component clearance, stencil access, and whether the panel can travel through the equipment with adequate support.
Board-specific checks matter. Open vias in soldering areas can draw solder away from a joint. Panel edges or tooling features can obstruct components, while fiducials need to remain visible to the placement system. EBest Circuit does not specify one universal rail width, clearance, or stencil thickness; those choices depend on the board and production setup.
From data review to post-reflow checks
Production starts with matching the bill of materials, footprints, placement coordinates, polarity marks, and assembly drawing. The board and components are then prepared, with part identity, packaging, and any moisture-sensitive handling requirements checked before printing.
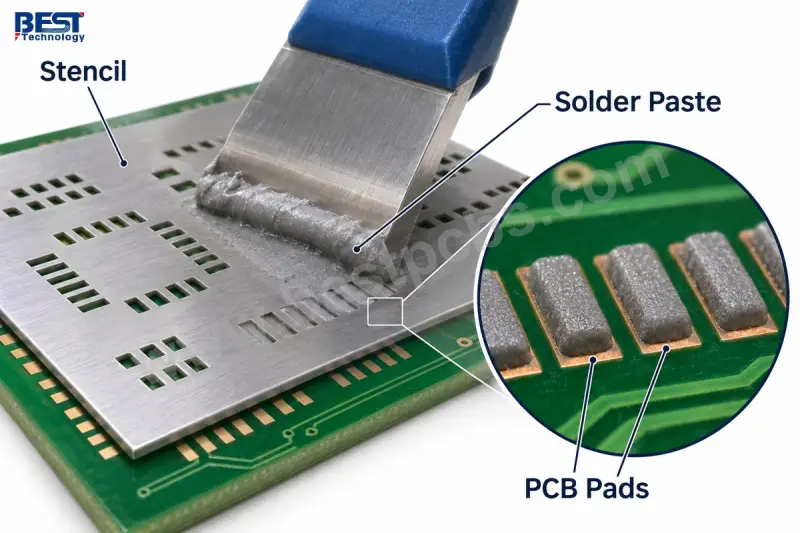
A stencil aligned to the PCB transfers solder paste through apertures onto the pads. Solder paste inspection (SPI) measures the deposits before components are placed. The placement system then positions parts at programmed coordinates, followed by reflow and post-solder checks. Detecting a print problem before placement can prevent it from continuing through the rest of the line.
For double-sided SMT, the sequence needs to account for component mass, package limits, and exposure to a second reflow cycle. Mixed assemblies also require a planned insertion and soldering method for through-hole parts, taking their heat limits into account.
Paste deposits and reflow profiles
Stencil thickness alone doesn’t determine print quality. Aperture size, shape, alignment, paste release, and stencil condition all influence the deposited volume. A board combining 01005 passives with a large power connector may need different paste volumes in different areas. Increasing stencil thickness to serve the connector could put too much paste on the small pads, so aperture adjustments or a stepped stencil may be considered.
SPI can assess paste height, area, volume, and offset. Repeated low-volume deposits may point to aperture release, contamination, board support, or print settings. Excess deposits and bridging call for a different investigation. The measurement is useful when it guides a process correction, rather than serving only as a pass/fail result.
For SAC305 lead-free solder, the stated example peak temperature is around 235–245°C. It isn’t a universal oven recipe. The paste specification, component temperature limits, and measured temperature profile on the actual board determine suitable settings. The profile considers ramp, soak where applicable, time above liquidus, peak, and cooling.
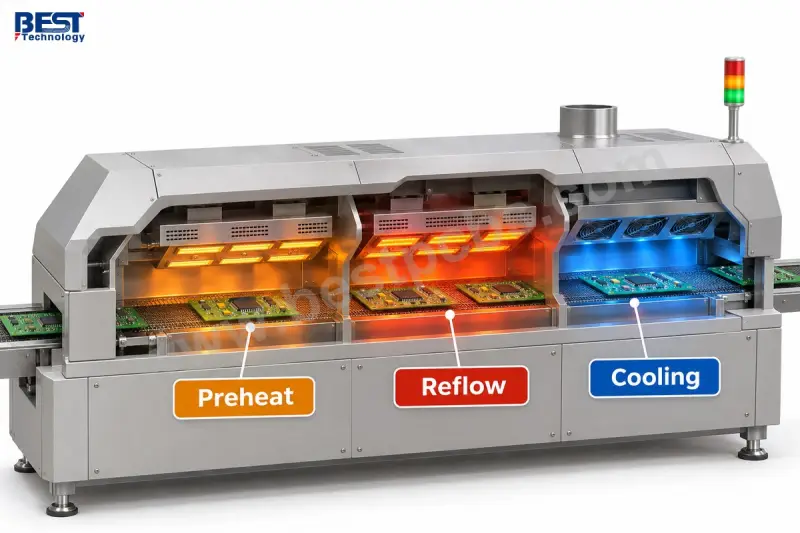
Thermocouples placed at locations with different thermal behavior can show whether a large copper area or heavy component heats more slowly than a small passive. An oven-zone setpoint is not the same as the temperature measured on the board. A different alloy and flux system may also require a different profile, even when the solder is lead-free.
Inspection and testing answer different questions
SPI checks paste before placement. Automated optical inspection (AOI) looks for visible assembly features such as component presence, position, polarity indicators, and visible solder-joint appearance. X-ray can examine hidden joints, including BGA connections, for issues such as bridging, solder distribution, and voiding where the selected technique can detect them. Functional testing checks circuit behavior defined in the test plan.
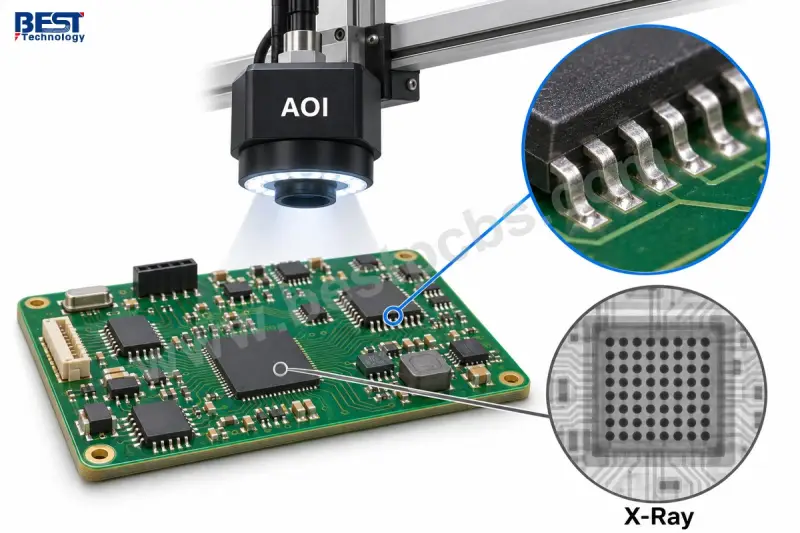
These methods are complementary. A clear top-side image can’t show every hidden joint, and an X-ray image can’t confirm that firmware or circuit behavior meets requirements. For BGA and QFN builds, inspection coverage and acceptance criteria should be agreed before production. Functional testing also needs a repeatable setup, including defined supply voltage, current limits, firmware version, fixtures, and expected responses. Applicable workmanship criteria are set with the customer rather than assumed to be the same for every assembly.
Defects point to different parts of the process. Bridging can involve excess paste, print offset, inadequate separation, or placement. Tombstoning can result from uneven wetting forces, heating, or paste deposits. Open joints may relate to insufficient paste, poor wetting, lifted leads, or warpage. QFN and BGA voiding can reflect the interaction of flux outgassing, stencil pattern, pad design, and reflow. The stated acceptance limit for voiding should fit the package, application, and agreed criteria; a single percentage doesn’t apply to every joint.
Cost, scheduling, and build readiness
Component availability, placement count, package difficulty, assembly sides, stencil needs, inspection coverage, and test preparation affect cost and schedule. A board with few parts can still take more planning if it uses a fine-pitch BGA or needs a custom test fixture. Prototype orders also spread stencil, programming, and setup work across fewer boards; unchanged repeat builds may reuse approved production data and tooling.
Cut-tape quantities, component attrition allowances, moisture-sensitive handling, and a second assembly side add preparation requirements. EBest Circuit says the schedule is confirmed after reviewing material availability and the manufacturing and test work. Customers can request assembly only, component sourcing, or a complete PCB and PCBA build, with consigned and partial turnkey options also available.
For a build review, the company requests Gerber files, the BOM, placement data, quantity, and test requirements. Those inputs let the team assess package-specific process needs and define the production scope before work begins. Prototype builds using production-relevant stencil, placement, reflow, and inspection methods can also provide a useful check of manufacturability ahead of volume production.
Common questions
What’s the difference between SMT and SMD? SMT means surface mount technology, the manufacturing method. SMD means surface mount device, the component mounted using that method. Printing paste and reflowing a chip resistor onto a PCB are steps in SMT assembly.
Can a board combine surface mount and through-hole parts? Yes. The insertion and soldering sequence is planned around the component mix and heat restrictions.
Can customers supply components? Yes. Consignment and partial turnkey builds are supported. Supplied parts need clear part-number identification, usable packaging, and enough quantity for setup and the agreed attrition allowance.
Does no-clean paste mean the board never needs cleaning? No. Cleaning depends on the qualified flux process and product requirements, including coating compatibility, sensitive circuitry, and residue acceptance. A no-clean designation doesn’t override a cleanliness specification.
Can prototypes use the same process as production? Yes, when the package mix and build requirements support it. Using production-relevant methods makes the prototype more useful for checking manufacturability before volume production.
 AMD Venice Uses 2.5D Packaging to Feed More Bandwidth Into EPYC Zen 6
 CNC Controller Board Design: Interfaces, PCB Specs and Assembly Testing
 Stratasys and Nano Dimension End $42.5 Million Markforged Sale Agreement