Automotive HDI PCBs: Manufacturing Controls, Reliability Tests and Supplier Selection
Automotive HDI board performance depends on the full stackup, microvia process, assembly handoff and traceable inspection plan—not a single feature-size claim.
Automotive HDI boards earn their place when fine-pitch packages, dense signal routing or limited board area make conventional through-hole fanout impractical. Their reliability depends on the whole manufacturing route: released stackup, microvia geometry, materials, assembly requirements and inspection records must stay aligned from prototype approval through repeat production.
That requirement spans ADAS controllers, automotive cameras, infotainment systems and vehicle communication modules. A supplier’s smallest advertised line or via dimension says little about whether it can reproduce the specified board. The useful question is whether its process and records match the design that was approved.
Where HDI construction helps
Microvias connect selected adjacent layers, opening routing channels for devices with high pin counts. In a compact camera module, for example, an image processor, memory and high-speed interfaces may need dense BGA escape routing. Domain and autonomous-driving controllers can call for controlled-impedance layers and short signal paths between processors and memory. Infotainment boards must fit processors, displays, storage and communication circuits into constrained space.
Automotive Ethernet gateways also benefit from careful impedance control, continuous reference planes and routing that accounts for connector transitions. Battery monitoring modules can use selective microvias to pack sensing and control circuitry into a small area, provided isolation and creepage requirements are maintained.
HDI is not the default answer for every circuit. High-current power distribution may be better served by wider conductors, heavier copper or a separate power board. Extra build-up layers add process steps and interfaces, so the construction should solve a specific routing or packaging constraint.
Define the construction before requesting a quote
A useful RFQ specifies the full construction and acceptance package. Include the layer stackup, layer-to-layer connections, copper weights, impedance table, material requirements, surface finish, panel constraints and required tests. A list of minimum feature sizes alone can lead to quotations based on different assumptions.
| RFQ field | Initial capability reference | Approval detail |
| Layer count and build-up | 2 to 16 layer HDI; 1+N+1, 2+N+2 and higher-order structures subject to review | Released stackup, lamination sequence, dielectric thicknesses and via connections |
| Laser microvia | 0.10 mm (4 mil) capability reference | Finished diameter, target and capture pads, dielectric depth and filling requirement |
| Fine line and space | 0.075/0.075 mm (3/3 mil) special capability reference | Copper thickness, finished conductor tolerance, plating route and inspection method |
| Microvia aspect ratio | 1:1 or lower is a common design target | Actual laminated dielectric thickness divided by finished microvia diameter |
| Materials | High-Tg FR-4, CAF-resistant or specified low-loss laminate | Manufacturer, grade, Tg, Dk/Df where relevant, thickness and substitution policy |
| Controlled impedance | Project-specific | Target, tolerance, layer, trace geometry, reference plane, coupon and report format |
| Surface finish | ENIG, ENEPIG, OSP or another approved finish | Finish thickness, solderability requirement, storage limit and assembly compatibility |
Microvia diameter only has meaning alongside dielectric depth and pad geometry. A nominal 0.10 mm laser microvia through a 0.075 mm dielectric gives an approximate depth-to-diameter ratio of 0.75:1. The released ratio should be calculated from the actual laminated stackup.
Control the failure modes at the process level
Microvia fatigue, layer misregistration, warpage, conductive anodic filament (CAF) exposure and via-in-pad planarity each need attention. A final continuity test can confirm that nets connect at the time of test, but it cannot establish long-term interconnect reliability or guarantee sound BGA solder joints.
- Microvia fatigue: Repeated thermal expansion can stress the interface between a microvia and its target pad. Geometry review, controlled drilling and plating, microsection evidence and specified thermal testing address different parts of the risk.
- Registration: Every sequential lamination cycle can shift features relative to earlier layers. Material compensation and in-process checks help keep each laser target within its released geometry.
- Warpage: Asymmetric build-ups and unbalanced copper can deform a panel during fabrication or reflow. Copper balance, material symmetry, lamination control and a defined flatness limit help manage it.
- CAF exposure: Moisture, electrical bias, spacing, material choice and drilling quality interact. CAF-resistant laminate does not remove the need for spacing and process controls.
- Via-in-pad solder loss: Incomplete filling, weak capping or uneven planarization can draw solder away from a BGA joint. Verify filling and surface planarity before assembly.
Stacked microvias add interfaces through the build-up. Where routing allows, staggered structures may reduce the number of stacked interfaces and simplify qualification.
Keep fabrication and assembly on the same data
The approved via map sets the number of lamination, laser drilling, metallization and filling cycles. The fabricator should establish that route before panel production: changing the stackup can affect impedance, registration, reliability, cost and schedule.
- DFM review: Resolve the stackup, via structure, copper thickness, material, impedance table, panel drawing and acceptance files before CAM release.
- Inner-layer fabrication: Form and inspect inner circuits, including buried-via subassemblies where the design calls for them.
- Sequential lamination: Add build-up layers under controlled pressure, temperature and registration conditions.
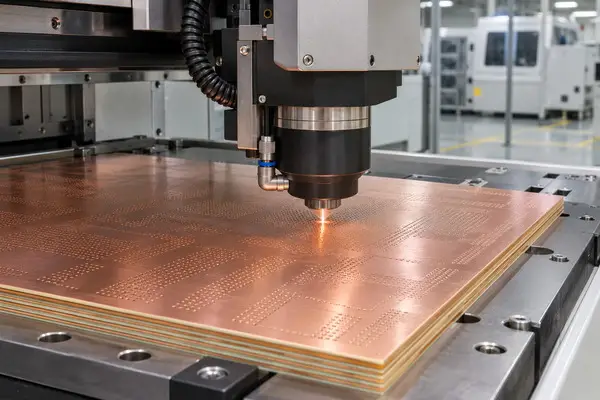
- Laser drilling and metallization: Drill the specified microvias, prepare the surfaces, then deposit and plate copper. Repeat for each additional build-up level.
- Filling and outer-layer completion: Fill and cap designated vias, form outer circuitry, then apply solder mask and surface finish.
- Bare-board inspection: Complete electrical testing and the specified dimensional, microsection, impedance and visual checks.
- SMT assembly: Apply solder paste, place components, reflow, inspect visible and hidden joints, then run agreed electrical or functional tests.
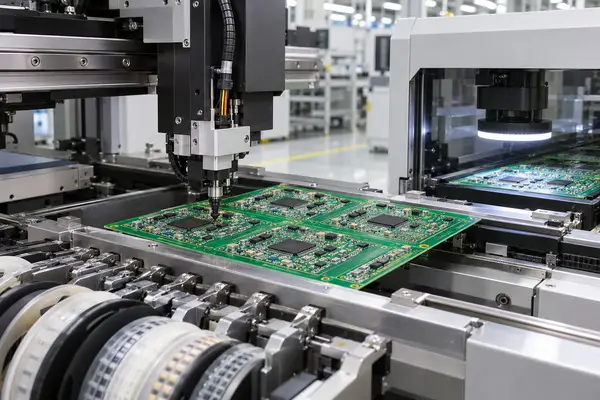
A board may pass continuity testing and still have via conditions or pad flatness that complicate BGA soldering. Fabrication and assembly teams should therefore review via-in-pad requirements against one released data package.
Match each test to a failure mode
The reliability plan should define what each test checks and the acceptance criteria. AOI, electrical test, microsection, impedance measurement, thermal exposure, X-ray and functional testing provide different evidence; they do not substitute for one another.
- AOI: Finds conductor pattern defects such as shorts, opens and etching anomalies at the relevant production stage.
- Electrical test: Checks continuity and isolation against the released netlist.
- Microsection analysis: Examines selected microvia interfaces, plated-hole structures, copper thickness and internal registration.
- Impedance measurement: Compares released coupon structures with the specified target and tolerance.
- Thermal stress or cycling: Applies a defined temperature profile and acceptance rule to the interconnections selected for qualification.
- IST, when specified: Tracks resistance change during repeated thermal loading on a defined coupon or structure.
- X-ray and functional testing: Inspects hidden assembly joints and checks the assembled module against the agreed test specification.
Passing an electrical test shows that a net is continuous at that moment. The qualification plan still needs to reflect the operating environment and customer requirements.
Check certificates and order-level records
Review the manufacturing site, certificate scope, order records and customer-specific approval package separately. A management-system certificate does not certify an individual board design or prove a particular process limit.
- Quality-management scope: IATF 16949 is an automotive quality-management-system standard aligned with ISO 9001. Check the current certificate, named site, scope, issuing body and validity.
- Bare-board requirements: IPC-6012F covers rigid printed board qualification and performance. The IPC-6012FA automotive addendum applies when procurement documents require the matching automotive requirements.
- Material traceability: Specify laminate and copper identification, lot records, required certificates and a Certificate of Conformance tied to the shipment.
- Inspection evidence: Define which electrical, impedance, microsection, dimensional, first-article and assembly reports must accompany the order.
- Production approval: Name PFMEA, Control Plan, PPAP level, approved samples and change-notification requirements when the customer program calls for them.
The purchase order and released drawing should identify the applicable standard revision and customer-specific acceptance rules. General capability statements do not replace those order-level requirements.
Compare suppliers against the same package
Supplier selection comes down to whether the proposed production route, quality controls, documentation and delivery plan fit the released design. Use the same RFQ package for every bidder; otherwise, a lower price may reflect a different stackup or inspection scope.
- Confirm the exact layer count, build-up, microvia type, copper weight, fine features and material grade.
- Ask how drilling, plating, via filling, registration, microsection sampling and specified thermal tests are controlled for the proposed construction.
- Match the manufacturing site to the certificate scope, process ownership, traceability route and customer requirements.
- Establish who owns via-in-pad planarity, stencil review, BGA inspection, rework limits and functional-test fixtures.
- Require one approved data package and written approval before changes to material, site, stackup, finish or process.
- Compare identical quantities, panelization, tests, documentation, tooling, components, freight terms and schedule assumptions.
- Check how approved materials, process parameters, inspection records and golden-sample references are retained for repeat orders.
- Define protective packaging, shipment splits, destination, Incoterm, shipping documents and delivery milestones.
The strongest fit is the supplier that can reproduce the approved construction with records that can be checked. A single advertised feature size is a much narrower measure of capability.
An illustrative eight-layer RFQ
The following values describe an illustrative quotation scenario, not a released customer case or proof of qualification for a particular vehicle program. It shows the inputs that need to remain consistent when a design uses multiple HDI build-up cycles.
| Input | Illustrative value | Release check |
| Construction | 8-layer rigid board with three HDI build-up stages | Complete layer and via map for each build-up cycle |
| Material | FR-4, Tg 180 class | Exact manufacturer, grade, thickness and substitution restriction |
| Finished thickness | 1.6 mm nominal | Finished tolerance and stackup calculation |
| Copper | 1 oz inner and outer layers | Definition of base copper versus finished plated copper |
| Via treatment | Specified resin-filled vias | Via list, fill type, capping, planarization and acceptance method |
| Surface finish | ENIG | Thickness requirement and compatibility with assembly and storage |
Before release, the manufacturing review should check registration through each lamination cycle, interactions between microvias and filled vias, panel movement, impedance geometry and required inspection samples. Use in an automotive program still requires customer-specific qualification and reliability evidence.
Understand cost and schedule drivers
Sequential lamination, via processing, fine features, materials, inspection, documentation and order quantity shape the quotation. A simpler construction that meets routing and reliability needs will generally involve fewer process steps and less yield exposure.
- Each sequential build-up adds imaging, lamination, laser drilling, metallization, inspection and yield exposure.
- Filled, stacked, skipped and via-in-pad features add process and acceptance requirements.
- Finished copper thickness and conductor tolerance affect whether 3/3 mil features suit the chosen layers.
- High-Tg, CAF-resistant and low-loss laminate grades differ in price, availability, storage and processing behavior.
- Extra coupons, thermal tests, first-article records, traceability, PPAP work and customer-specific documentation add cost when required.
- Tooling, setup, test programming, panel utilization, attrition and component procurement affect prototype and volume orders differently.
Lead time should be confirmed after DFM. Stackup release, material availability, test scope, assembly and approval steps all affect the schedule. A project plan should show data release, material readiness, fabrication, assembly, approval evidence and shipment, and state which milestone starts the committed lead time.
Material procurement can move the start date when the design calls for named laminate grades, copper weights, finishes or long-lead components. Additional lamination and microvia cycles add operations and inspection holds. Assembly brings its own dependencies, including component availability, stencil review, BGA inspection, programming, fixtures and functional testing. First-article review, PPAP, reliability testing or deviation approval may extend the customer approval sequence beyond manufacturing. Packaging, split shipments, freight booking, shipping documents and destination transit also need their own schedule.
Order details that prevent avoidable ambiguity
Confidential files can be shared under an NDA requested before transfer; the agreement should identify any affiliated sites or subcontracted processes it covers. If the design requires a particular laminate manufacturer, specify its grade, thickness, copper construction and substitution policy, then confirm availability and process compatibility.
For consigned components, provide the BOM, quantities, packaging, date-code or traceability requirements, moisture-sensitivity status and permitted attrition. The quotation should define responsibility for shortages and damaged parts. Serial numbers and barcodes should be specified by format, location, size, contrast, serialization source, duplicate-prevention method and readability check.
Custom assembly panels need approved fabrication and assembly drawings covering rails, fiducials, tooling holes, board spacing, support, depaneling and SMT handling. Split shipments should identify quantities, destinations, dates, lot identity, packaging, freight responsibility and the records accompanying each batch. Custom overseas packaging should define board separation, ESD protection, moisture barrier, desiccant, humidity indication, vacuum sealing, carton labels and pallet limits.
For a reorder, confirm that the released revision, materials, construction, process route, acceptance criteria and approved deviations remain valid. Any proposed change should identify the affected part and revision, the material, process, site, equipment or sub-tier involved, the reason, risk review, validation plan, timing and required customer approval. Retained samples or coupons should be linked to a production lot and inspection record, with type, quantity, storage conditions, retention period and release or disposal authority defined in the order.
For a project-specific quote, provide Gerber or ODB++ data, the released stackup and via map, impedance table, BOM, quantity, panel or assembly requirements, approved materials, firmware or programming method, test specification, documentation package, delivery location and required milestones. EBest Circuit describes its offer as combining HDI fabrication, component sourcing, SMT assembly, inspection and project documentation; final capability and records should be confirmed against the released files and quotation. The same review should distinguish mandatory customer requirements from optional tests and documentation.
 AMD Venice Uses 2.5D Packaging to Feed More Bandwidth Into EPYC Zen 6
 CNC Controller Board Design: Interfaces, PCB Specs and Assembly Testing
 Stratasys and Nano Dimension End $42.5 Million Markforged Sale Agreement