Precision CNC Grinding: Controlling Surface Integrity, Geometry and Inspection
CNC grinding can refine hardened parts to tight dimensions, but wheel condition, heat control, workholding and inspection determine the result.
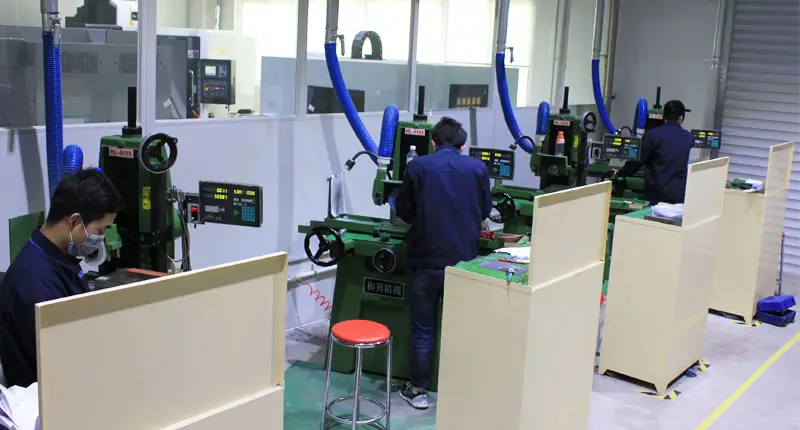
Precision CNC grinding earns its place in a manufacturing route when the finished part needs more control over size, form or surface texture than earlier machining can provide. It is often used after heat treatment, when hardened steel is difficult to finish with conventional cutting tools. The process can also handle tool steels, stainless steels, carbide and other difficult-to-machine materials.
That accuracy depends on the whole process, not simply on choosing a fine wheel. Machine condition, workholding, wheel dressing, cutting parameters, coolant delivery and measurement all affect the finished component. A part may meet its nominal dimension yet still have poor geometry or heat damage beneath an apparently acceptable surface.
What the grinding process controls
A grinding wheel rotates against the workpiece, and its many abrasive grains act as small cutting edges. CNC control programs the wheel’s position and movement, along with feed rates, depth of cut and machining sequence. This lets manufacturers remove small, controlled amounts of material and repeat the operation consistently.
The specific method depends on the part: surface grinding produces flat faces; cylindrical and internal grinding address external and internal diameters; profile grinding follows more complex contours. Grinding may be used to correct dimensions after heat treatment, refine a functional surface or establish geometric relationships between features.
Its value is clearest where the part needs tight dimensional tolerances, low roughness, flatness, roundness or a controlled fit with a mating component. If milling or turning can meet the drawing requirements, adding grinding may add time and cost without improving the part’s function. The choice belongs in the overall process plan.
Surface condition goes beyond roughness
Surface roughness is a common specification, but it describes only the texture of the surface. Grinding also affects the material at and just below that surface. Thermal and mechanical effects can matter even when a measured Ra value meets the drawing requirement.
The achievable finish depends on the abrasive and wheel specification, dressing condition, process settings, workpiece material and coolant performance. Bearing surfaces, sliding interfaces, seals and precision tooling may need a defined texture for their intended function. A drawing should state a roughness requirement where one matters; “smooth finish” leaves the target open to interpretation.
Grinding burn is a key risk. Heat concentrated in the grinding zone can alter hardness, residual stress or other metallurgical properties, and may cause discoloration. Excessive grinding depth, a wheel in poor condition, inadequate coolant delivery, high feed or insufficient dressing can contribute. For critical parts, process control must consider the material condition as well as the measured dimensions.
Residual stresses can also change during grinding. Their effect depends on the workpiece material, wheel, cooling strategy and heat generated. For components where fatigue performance or dimensional stability matters, process development needs to account for these surface effects rather than treating grinding as a purely geometric operation.
Geometry depends on the setup
Dimensional accuracy does not guarantee geometric accuracy. Flatness, parallelism, perpendicularity, roundness, cylindricity and concentricity describe different aspects of a part’s form and feature relationships.
Surface grinding is often used to establish a flat reference face, but the result can be affected by machine rigidity, wheel dressing, chuck condition, machining sequence and heat. Thin or flexible workpieces need particular care: clamping and grinding forces can deform them while material is being removed, so the measured shape after release may differ from the shape under restraint.
Parallel faces require control of their relationship as well as their individual thicknesses. Grinding both faces can help, provided the workholding and sequence are suitable. For shafts, bearing seats, pins and sleeves, cylindrical grinding can control diameter and form together. Alignment, workholding, wheel condition and machine performance all influence roundness and cylindricity.
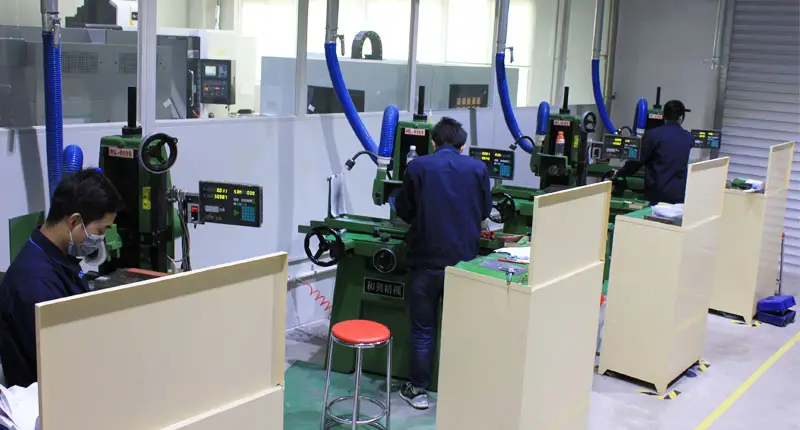
Wheel, coolant and machine condition
Wheel selection should match the workpiece material, grinding operation, target finish and required material removal. Abrasive type, grain size, hardness grade, structure and bond all affect cutting behaviour. A wheel that is too hard may retain worn grains instead of releasing them; a poorly matched specification can reduce cutting efficiency or increase heat.
Dressing restores the wheel’s cutting condition and can clear loaded or worn abrasive. Because wheel performance changes during production, dressing has a direct role in maintaining consistent results. The right interval and method depend on the operation and the wheel.
Coolant helps remove heat and grinding debris, but flow alone does not guarantee effective cooling. The fluid needs to reach the contact zone; nozzle position, pressure, flow, filtration and fluid condition all play a part. Temperature changes in the workpiece, machine or wheel can cause dimensional variation, which is why stable machine temperatures and shop conditions matter for close tolerances.
Workholding must support the part without distorting it. Magnetic chucks are commonly used for ferromagnetic work during surface grinding; non-magnetic materials and complex shapes may need other fixtures. Vibration, spindle runout, machine deflection or poor maintenance can produce chatter, uneven patterns, size variation and poor finish. Machine maintenance and calibration are therefore part of process quality.
Parameters and troubleshooting
Wheel speed, workpiece speed, feed, grinding depth and material removed per pass need to suit the material, geometry, wheel and tolerance. Roughing and finishing often use different strategies: roughing removes material efficiently, while finishing controls the final size and surface. Large cuts can add heat; excessively cautious settings can reduce productivity without improving quality. The aim is a stable balance between removal rate, geometry, finish and thermal control.
Chatter may point to vibration from the machine, wheel balance, parameters or workholding. Burn suggests excessive thermal loading and can call for attention to wheel condition, dressing, coolant or cut settings. Taper and uneven dimensions may stem from alignment, workholding, wheel wear or changing process conditions. Wheel loading can lower cutting efficiency and add heat.
Troubleshooting is more effective when the likely cause is isolated across the machine, wheel, workpiece, process, coolant system and measurement method. Changing several variables at once makes it harder to identify what corrected the problem.
Inspection and drawing requirements
Visual checks cannot verify many grinding requirements. Micrometers, precision gauges and height gauges can measure dimensions; coordinate measuring machines can check multiple features and their relationships. Dedicated roughness instruments assess specified surface parameters, while specialized equipment can measure roundness and cylindricity. Critical parts may also need examination for burn, cracks or other surface defects. The method depends on the material, application and specification.
A useful drawing identifies which features require grinding and defines their dimensional tolerances, roughness and geometric tolerances. It should also state the required hardness or heat-treatment condition where applicable. For demanding parts, specify any additional surface integrity checks and the inspection method. Clear requirements give the manufacturer a basis for choosing both the process and the means of verifying it.
Precision grinding is most effective when the process plan controls the part’s geometry and material surface together. Matching the wheel and setup to the component, managing heat and verifying the specified features makes grinding a purposeful final operation, especially after heat treatment.
 AMD Venice Uses 2.5D Packaging to Feed More Bandwidth Into EPYC Zen 6
 CNC Controller Board Design: Interfaces, PCB Specs and Assembly Testing
 Stratasys and Nano Dimension End $42.5 Million Markforged Sale Agreement