Custom SiC Gate Driver Board Manufacturing: PCB Limits, Assembly and Testing
A custom SiC gate driver build depends on preserving isolation geometry and matching PCB construction, components, inspection and testing to the approved design.
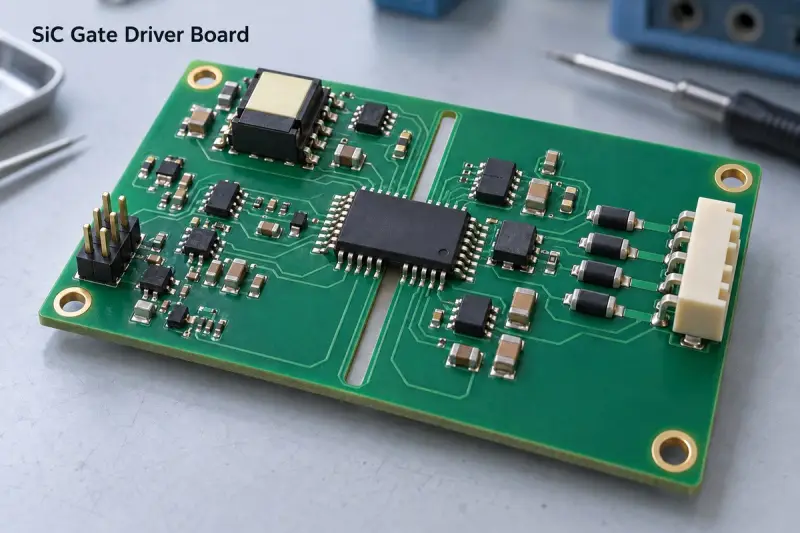
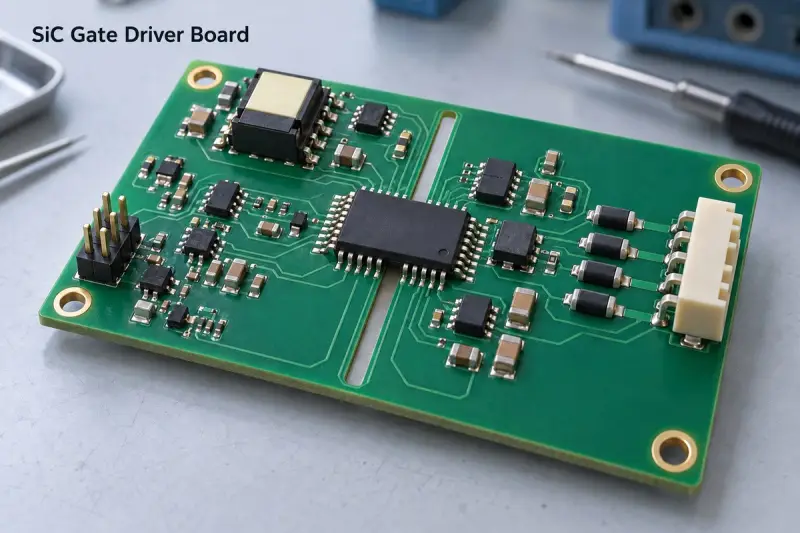
A custom silicon carbide (SiC) gate driver board has to do two jobs at once: carry the control circuitry for a power device and preserve the physical separation required by its insulation design. Manufacturing therefore depends on more than producing a board that matches the outline. Layer construction, copper weight, holes, slots, assembly details and inspection scope all need to agree with the approved design.
EBest Circuit offers PCB fabrication, component sourcing, SMT and through-hole assembly, and project-specific functional testing for customer-designed boards. The service can cover bare PCBs, assembled prototypes and later production builds. Its manufacturing review uses the project’s fabrication data, bill of materials (BOM), quantities and testing requirements to establish a production scope.
Choose the board around the power stage
Gate driver layouts vary with the switching device and the equipment around it. A single-channel board may serve one specified switch. A half-bridge design needs separate high-side and low-side drive paths. A board for a SiC power module must match that module’s interface, while an integrated design may combine gate-drive circuitry with other board functions.
These configurations call for different interfaces and assembly details. Isolated power supplies, gate resistors, connectors and protection components belong in the build where the approved BOM specifies them. Fabricating and assembling a board does not, by itself, demonstrate that the finished converter meets its operating requirements.
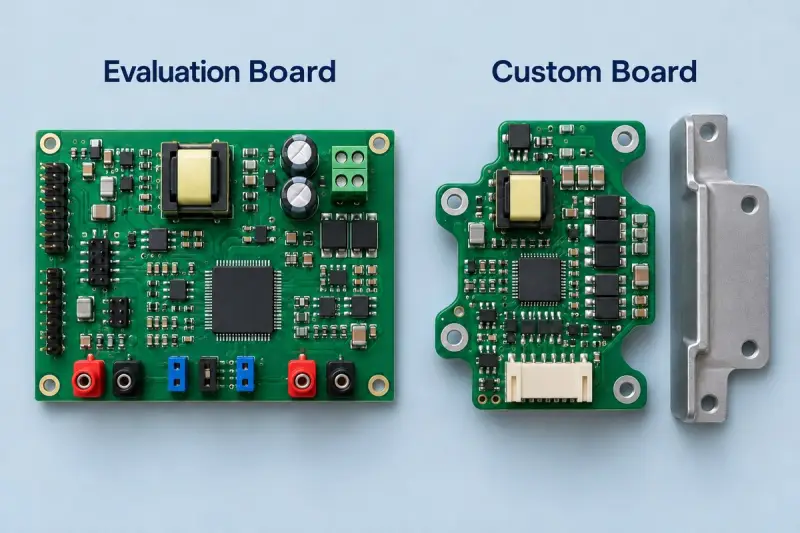
The choice between an evaluation board and a custom design is largely a question of fit and control. Evaluation boards provide a predefined circuit and mechanical interface for device assessment and application development. A custom board can match the equipment’s outline, connector locations, circuit configuration and production documentation. That can matter when the board must connect to a particular power module or fit an existing assembly.
An evaluation board can remain useful beyond initial development if it suits the end application and passes the necessary assessment. Custom manufacturing takes engineering and validation effort, so it does not guarantee lower cost or better performance. Its value is in adapting the hardware and manufacturing files to a defined product and repeat-build plan.
PCB capabilities and their limits
EBest Circuit lists standard PCB fabrication from 1–10 layers and special processing from 10–32 layers. Material options include low-Tg FR4 at 130–140°C, mid-Tg material at 150°C, and high-Tg material at 170–180°C. The stated copper ranges are 0.5–5 oz for standard inner layers and 1–5 oz for standard outer layers.
At 1 oz copper, the minimum outer-layer trace width and spacing are 4/4 mil under standard processing and 3/3 mil with special processing. Minimum finished hole diameter is 0.20 mm standard or 0.15 mm special. Standard tolerances include ±3 mil for plated-through-hole diameter, ±5 mil for board outline, and ±4 mil for non-plated slot length and width.
Board thickness depends partly on surface finish. For OSP, ENIG, immersion silver, immersion tin and ENEPIG, the listed range is 0.4–3.5 mm; for HASL it is 0.6–3.5 mm. Available finishes are OSP, ENIG, ENEPIG, immersion silver, immersion tin and HASL.
These figures describe capabilities, not a set of limits that can all be combined freely. Layer count, copper weight, hole size and finished thickness interact. The documented process requires high-Tg material for boards with eight or more layers, and the selected layer construction constrains achievable thickness. A design review needs to assess the complete construction against the chosen process.
Fine manufacturing spacing also does not establish an adequate electrical insulation distance. The trace spacing a fabricator can produce may be much smaller than the separation needed between isolated circuits. That geometry must follow the insulation design and remain intact through fabrication.
Material, stackup and isolation geometry
Standard FR4 may suit a design whose thermal and insulation requirements fit conventional glass-reinforced epoxy. High-Tg FR4 offers a higher glass-transition temperature and is required by the stated process for eight-layer and higher boards. Special processing also lists higher-CTI laminate options from CTI 400–600 for designs that specify a particular tracking-resistance material class.
Two-layer construction limits routing and reference-plane choices. Four layers provide additional routing and reference-plane allocation, which may help compact designs manage return paths. More layers can support denser interconnections or several channels, but layer count alone does not improve the driver’s electrical behavior.
Stackup decisions need to account for operating conditions, copper thickness, board thickness and insulation needs together. Tg is a material property, not a continuous operating-temperature rating. Selection also needs to reflect actual temperature exposure, assembly conditions and other relevant thermal properties.
Creepage and clearance requirements depend on the insulation design, voltage conditions, environment and material properties. Copper, vias and other conductive features must respect the isolation zones on every relevant layer. Slots can form part of that geometry, so a manufacturing review should preserve their approved dimensions and position.
Manufacturing review can identify conflicts between a layout and the fabricator’s process, including fine copper features, holes, slots, board edges and component footprints. It can also check solder access, polarity markings, exposed pads, panel tooling, board support and depaneling locations. Those checks help make the assembly inspectable and manageable, particularly near connectors and edge-mounted parts.
Some layout features remain electrical design decisions. Gate-loop geometry, Kelvin-source connections and protection timing can affect circuit behavior. If a manufacturing change touches one of these areas, the design owner needs to assess and approve it before production.
Assembly and sourcing
EBest Circuit supports turnkey, partial-turnkey and consigned assembly. The process can combine SMT components with through-hole connectors and other leaded parts. For turnkey work, PCB fabrication, procurement, assembly and agreed inspection can be coordinated against the same approved revision.
Component sourcing is based on the approved BOM, with incoming material checks. A proposed substitute requires approval before use. Matching a replacement part’s footprint is not enough: a different driver IC or protection component may change drive characteristics, protection behavior or isolation specifications. The design may need validation against the selected substitute.
For SMT assembly, the listed process includes stencil printing, solder paste inspection, component placement and reflow soldering. Reflow profiling is set for the actual assembly. Through-hole parts use the selected soldering process, and mixed-technology boards can pass through both surface-mount and leaded assembly steps.
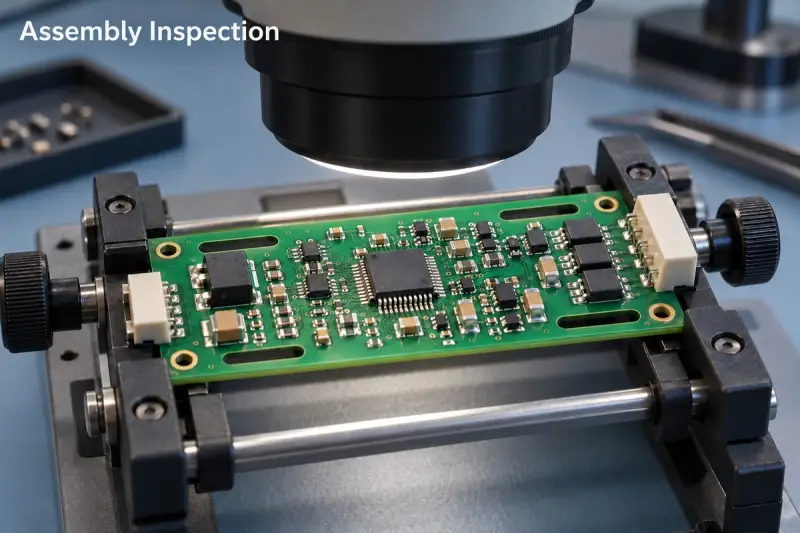
Inspection methods address different features. Automated optical inspection (AOI) can check visible assembly characteristics such as missing parts, polarity and detectable solder defects. X-ray inspection is available for selected packages with hidden connections, including applicable BGA and bottom-terminated parts. AOI cannot reveal internal joint features that are hidden from view, while X-ray provides information about those concealed connections.
Coordinating fabrication and assembly helps resolve issues involving footprints, board finish and component handling across production stages. It also gives customers one project scope to manage from bare board through completed PCBA, while retaining options to supply selected components themselves.
Inspection and the boundary of functional testing
The documented quality equipment includes bare-board electrical testers, flying-probe equipment, 3D solder paste inspection (SPI), 3D AOI and an AX8200 X-ray inspection system. Bare-board electrical testing checks for opens and shorts against the board’s electrical data before assembly. Visual inspection can be used at incoming, in-process and final stages.
SPI measures paste deposition, including volume, area and height, after printing and before placement. First-article inspection checks component values, placement and assembly conformity during initial setup. AOI checks optically accessible features after soldering, and X-ray can assess selected hidden connections for characteristics such as bridging and voiding.
Functional testing uses an agreed procedure, suitable equipment and acceptance criteria. Its scope needs to be defined for the project; a test that checks specified board responses does not necessarily validate the full power stage. System-level insulation testing, double-pulse testing and short-circuit protection validation are not included by default. Any such work requires separately confirmed facilities, procedures and responsibilities.
Cost, schedule and production planning
Quotation and lead time depend on the PCB build as well as the circuit’s parts and assembly plan. Availability of isolated driver ICs, DC-DC converters and protection components can affect purchasing schedules. High-CTI laminate, extra layers or special processing can change material availability and fabrication routing.
Tight hole, slot or outline tolerances may need added process review, particularly when the board mates with a power module or connector assembly. Mixed SMT and through-hole work, hidden-joint inspection and extra handling also affect production effort. A first build may require setup for functional tests or dedicated fixtures.
Prototype and production quantities distribute setup costs differently, and component purchasing quantities affect unit cost. Comparing quotations is useful only when the fabrication, procurement, assembly, inspection and test scopes are comparable. A lower quoted unit cost may reflect a different scope rather than a more efficient way to deliver the same board.
Preparing a manufacturing package
A useful review starts with revision-controlled fabrication data, drill files and a board drawing. Include the required stackup, laminate, copper thickness, surface finish and critical dimensions. For assembly, provide the BOM, placement data and drawings, including a clear list of positions that should remain unpopulated.
State the intended quantity and whether components will be supplied by EBest Circuit, the customer or both. Include the required delivery date, acceptance criteria, functional test procedure and fixture requirements. Clear revision identification helps engineering and procurement assess the same design and lets the quotation specify the applicable process and inspection scope before production release.
Common design-transfer questions
Does every board need conformal coating? No. The decision depends on environmental exposure and the insulation strategy. Coating does not automatically allow shorter creepage or clearance distances.
Can customer-supplied driver ICs be assembled? Yes. Consigned and partial-turnkey arrangements can include customer-supplied parts, with incoming checks and handling matched to the approved components and packaging.
Can isolation slots be changed during manufacturing? Changes to isolation geometry need approval from the design owner. If a slot cannot be produced as drawn, the proposed revision needs review for manufacturability and its effect on the insulation design.
Can one board support several component variants? It can when the design allows them. Each version needs a distinct assembly BOM, unpopulated-position list and test configuration so parts are not mixed between builds.
Can all SiC MOSFETs use the same gate-drive voltage? No. Recommended drive levels and absolute gate-voltage limits depend on the selected device. The driver supply and associated components need to follow that device’s requirements.
For a project review, send Gerber files, the BOM, build quantities and testing scope to [email protected]. Those details give EBest Circuit a basis to assess the board construction, assembly plan and agreed checks for a custom SiC gate driver board.
 AMD Venice Uses 2.5D Packaging to Feed More Bandwidth Into EPYC Zen 6
 CNC Controller Board Design: Interfaces, PCB Specs and Assembly Testing
 Stratasys and Nano Dimension End $42.5 Million Markforged Sale Agreement