TR7700Q Pairs Bottom-Side 2D and Top-Side 3D AOI for Double-Sided PCBs
TRI's TR7700Q TB SII checks PCB tops in 3D and bottoms in 2D, with 10 µm high-resolution settings and boards up to 510 × 510 mm.
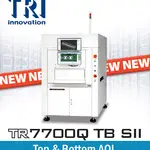
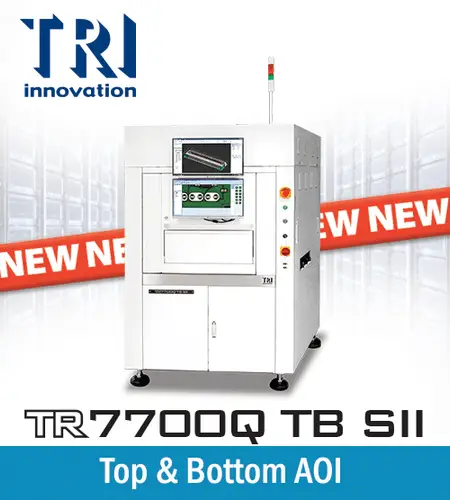
Test Research, Inc. (TRI) has launched the TR7700Q TB SII, a dual-sided Automated Optical Inspection (AOI) system. The top side gets 3D inspection and the bottom side gets 2D inspection, so one machine covers both faces of an assembled board. For lines that populate both sides, that's a meaningful change in how inspection gets scheduled and fixtured.
Why split 2D and 3D across the two faces
Height data is where most of the value sits on the top side. Tall components, lifted leads, tilted packages and solder fillets all show up as height errors that a flat 2D image can miss or misread. On the bottom side, the typical problems are different: missing or misaligned parts, solder bridging, and joint presence and shape. Many of those are visible in 2D with good illumination and colour, so the TR7700Q puts the 3D hardware on top and keeps the bottom view 2D. That split tends to match how assemblies actually fail, though the real test is whether a given product's defect mix justifies the extra hardware on the bottom.
How the 3D measurement works
TRI says the system uses Quad Digital Fringe Projectors. This is a fringe-projection approach, and the principle is straightforward. A projector throws a pattern of light stripes onto the board. Where the surface is flat, the stripes stay evenly spaced. Where a component rises above the board, or a joint is domed or sagging, the stripes shift and bend. Cameras record that distortion, and software converts the phase shift into height at each point. Using four projectors rather than one is typically done to cover shadowed areas and reduce occlusion around tall parts, which is exactly where a single viewing angle struggles.

The company describes this as metrology-grade measurement, meaning the system can measure component dimensions, positions and other physical characteristics, not just flag whether something looks wrong. That distinction matters if you're using the data for process control and not only pass/fail sorting.
Lighting, colour and the resolution trade-off
The system steps through several phases of LED illumination to capture features under different lighting conditions. This is a common technique for dealing with specular reflections from solder and metallic finishes, which can wash out or hide detail under a single light angle. TRI adds true-colour imaging, which it says helps separate components, solder joints and other board features by their actual colours. The company notes this helps when parts have different surface finishes. Colour-based separation is a practical advantage, though it still depends on consistent lighting and a sensible programme for each part family.
Resolution is set per side, and the figures show the trade-off clearly:
High-resolution setting: 10 µm top / 10 µm bottom.
High-speed setting: 15 µm top / 12.5 µm bottom.
Throughput is given as image capture and processing at up to 57 cm² per second. Choosing between the two settings means deciding whether fine-pitch detail or cycle time is the bottleneck on a given line. A fine-pitch board with small passives and tight-pitch leads will usually justify the high-resolution mode. A board with larger parts and more forgiving tolerances may run faster without giving up anything meaningful, though that call should be made with real defect data.
Programming and setup
TRI describes AI-powered algorithms for defect identification, along with smart programming tools intended to reduce the effort of setting up the machine for each new PCB design. In a high-mix environment, programming time often matters as much as cycle time, because every changeover takes the line off the clock. The company says the tools reduce programming effort, but it hasn't published details on how much time that saves, so any real-world gain will need to be measured on your own boards.

The company claims the system checks a wide range of component placement, orientation, soldering and assembly defects. It also says the solution verifies whether components are correctly positioned and whether pins and solder joints meet manufacturing requirements. Those are broad claims, and the defect coverage you get will depend on the specific parts and joint types on your board.
Mechanical limits that shape fixturing
The mechanical specifications are where many integrators will start. The stated maximum 3D height is 40 mm. Top clearance is 50 mm and bottom clearance is 40 mm, for PCBs up to 510 × 510 mm. Those clearances are what decide whether a tall connector, heatsink or shielded can on the top side, or a press-fit or through-hole lead protruding on the bottom, will fit without modification. Check the board's tallest and lowest features against these numbers before assuming the machine can handle a given assembly, and confirm the figures with TRI for your exact configuration.
What to watch next
The interesting question is whether dual-sided AOI in a single machine becomes a default choice or stays a niche for lines with heavy double-sided assembly. My read is that it's most useful where the bottom side carries parts that are hard to access later, because catching a bottom defect before the board moves downstream is cheaper than finding it at test. Until there are independent measurements of throughput and defect escape rates on real production boards, treat the numbers above as the manufacturer's specifications and plan a trial run on your own product before committing.
 ProMateria Opens Metal Additive Plant, Starting With GMH Spare Parts
 Q.ANT's Photonic NPU Runs Fourier Transforms in Light for AI Workloads
 SiTime's FemtoClock 4 and VersaClock 8 Target AI Data Centre Timing